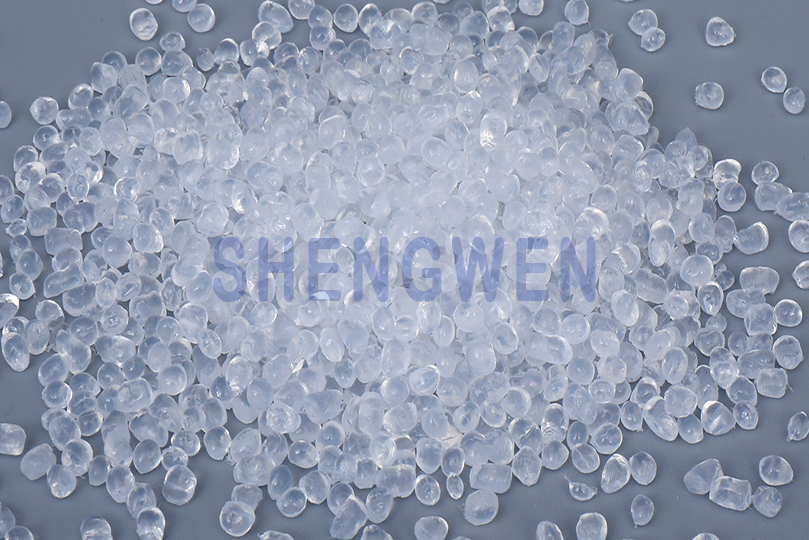
PEBA is a thermoplastic elastomer used in components that require flexibility, low weight, and reliable performance across different operating conditions. Achieving consistent molded parts depends on matching the resin grade to the application and maintaining stable processing conditions.
The following guide covers key preparation steps, injection molding adjustments, and common defects to check before production.
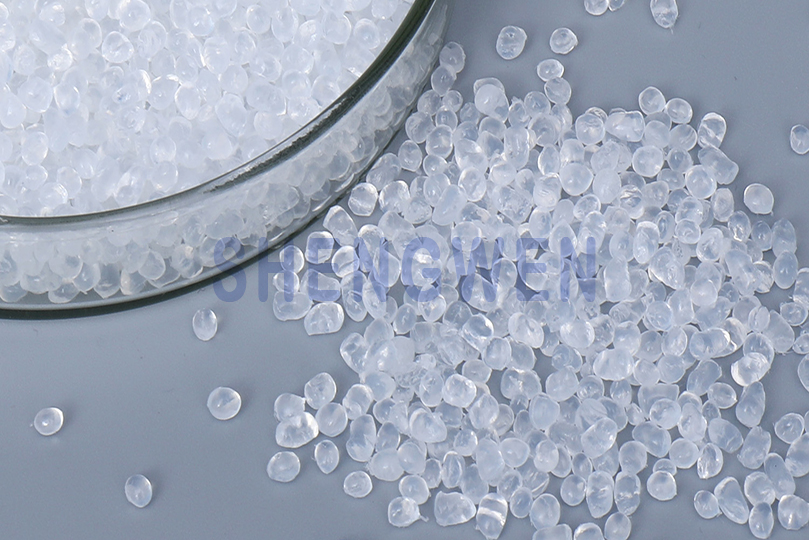
PEBA grades vary in hardness, density, and flexibility. Tuntun Plastic offers PEBA materials in a range of Shore D hardness grades, including 25D, 40D, 50D, 55D, 62D, 70D, and 72D, to meet different application requirements.
Consider the required flexibility, operating temperature, and intended application before choosing a grade. The PEBA material page provides product specifications for comparing available options.
PEBA absorbs moisture, so the resin should be dried according to the requirements of the selected grade before molding. Inadequate drying may cause surface defects and affect the quality of molded parts.
Use suitable drying equipment, follow the manufacturer's instructions, and keep unused pellets sealed to limit moisture exposure during storage and handling.
Melt temperature affects material flow and cavity filling. If the temperature is too low, the melt may not fill the mold completely. Excessive heat or prolonged residence time may increase the risk of material degradation.
Follow the recommendations for the specific grade and check filling performance during initial trials. Adjust the temperature gradually rather than applying one setting to every PEBA grade.
Injection speed and pressure influence filling consistency and surface quality. Insufficient filling may leave incomplete sections, while excessive pressure can contribute to flash and other molding defects.
Adjust these settings according to part geometry, wall thickness, and mold design. Check the finished parts before confirming the production settings.
Mold temperature affects cooling behavior, surface appearance, and dimensional consistency. Uneven cooling can lead to deformation or variation between molded parts.
Maintain stable mold conditions and evaluate the finished parts for dimensions and surface quality during trial runs.
Silver streaks, bubbles, or other surface imperfections may indicate moisture problems or unsuitable processing conditions. Review material drying, temperature settings, and mold venting before changing several parameters at once.
Flash and incomplete filling can result from unsuitable injection settings, mold conditions, or venting problems. Inspect the mold and adjust the relevant settings systematically to identify the cause.
For additional guidance on matching material properties to application requirements, see the PEBA material selection guide.
Drying temperature, drying time, injection temperature, and mold temperature vary by PEBA grade and processing equipment. The manufacturer's PEBA technical data sheet provides reference conditions for different hardness ranges.
These parameters are for reference only and should not be treated as universal production settings. Contact the supplier to confirm the appropriate conditions for the selected grade, then validate them through actual molding trials before mass production.
Yes. Dry PEBA resin according to the selected grade's requirements to help reduce moisture related defects, such as silver streaks and bubbles.
The appropriate temperature depends on the PEBA grade and processing equipment. Refer to the manufacturer's technical data sheet and validate the settings through molding trials.
Consider the required hardness, flexibility, operating conditions, and end use. Compare product specifications and consult the supplier to confirm the suitable grade.
Consistent PEBA molding requires suitable grade selection, proper drying, and controlled injection conditions. For grade specifications or processing support, please contact us. Our team can help confirm the right PEBA grade for your application and provide guidance on parameter validation before mass production.
By continuing to use the site you agree to our privacy policy Terms and Conditions.